Tested, not assumed
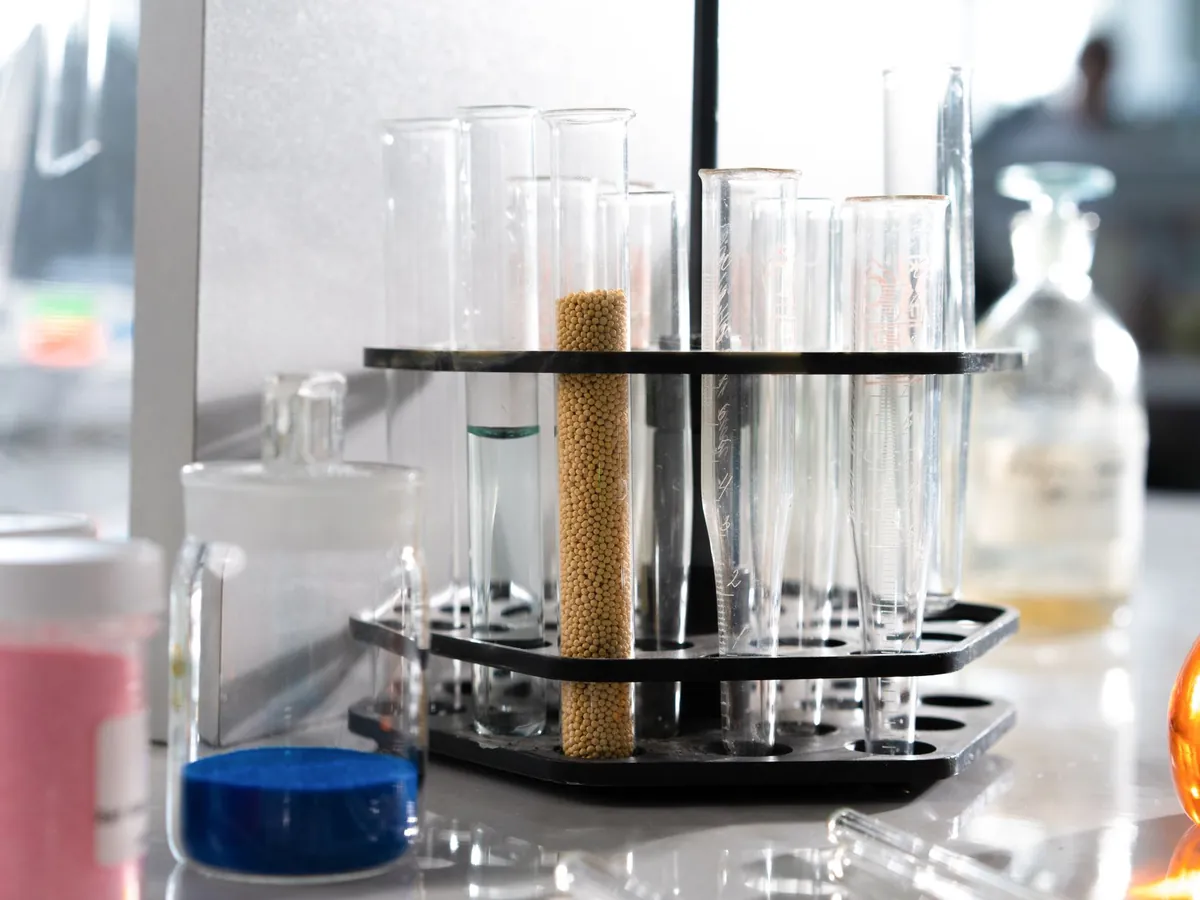
Every batch is sampled and cube-tested. The certificate that reaches your site is for the cement on the truck.
About us
Bastion started in 1998 with a single kiln and a rule we still keep: nothing leaves the plant until the lab signs it off. Today we mill eleven thousand tonnes a month and deliver to sites across the region.
HomeAbout us
Every batch is sampled and cube-tested. The certificate that reaches your site is for the cement on the truck.
Our blended cements replace up to 35% of clinker with fly ash and slag. Each product page states what that saves.
A named sales engineer for every trade account, and a dispatch desk that tells you where your truck is.
How we work
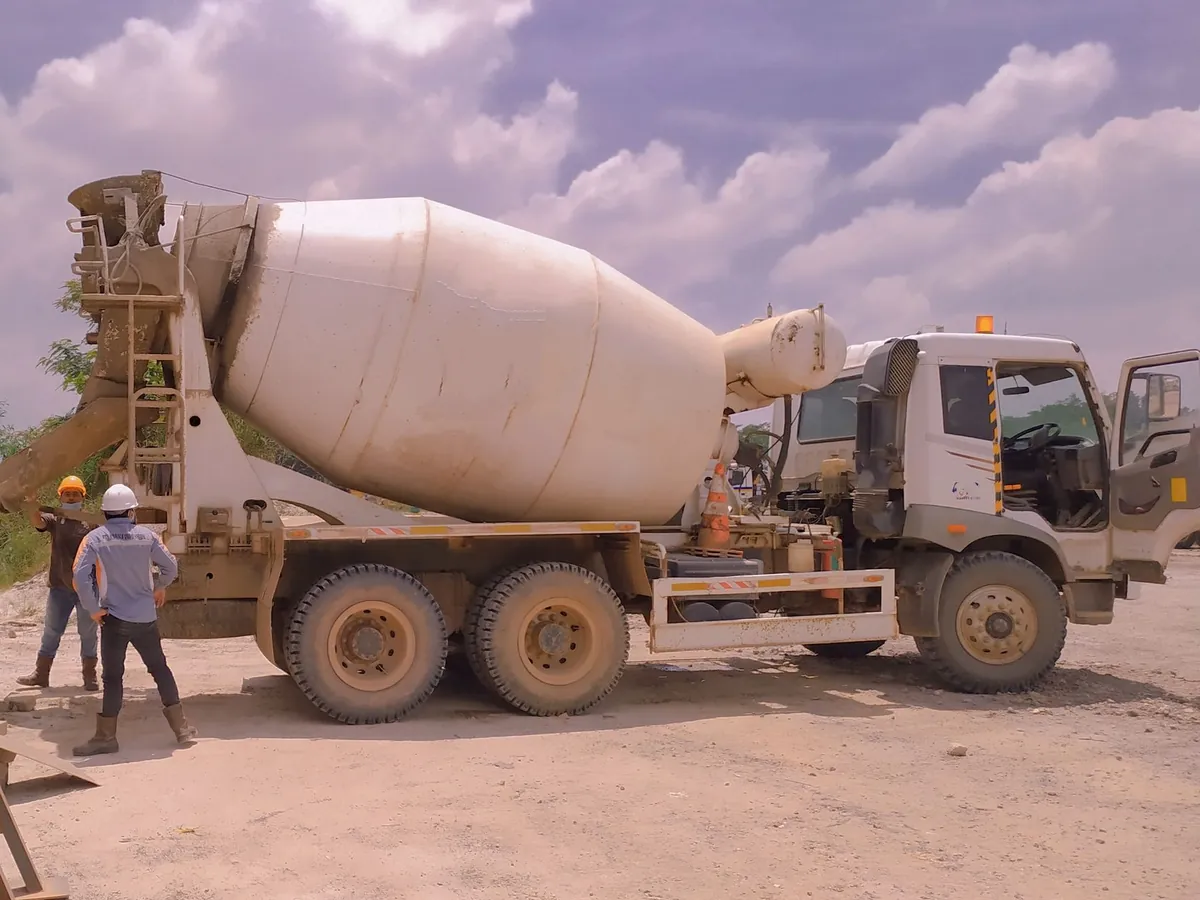
From quarry to site
Limestone and clay are quarried next to the plant, crushed and blended to a fixed recipe.
The raw meal is fired at 1,450°C into clinker, then cooled fast to lock in strength.
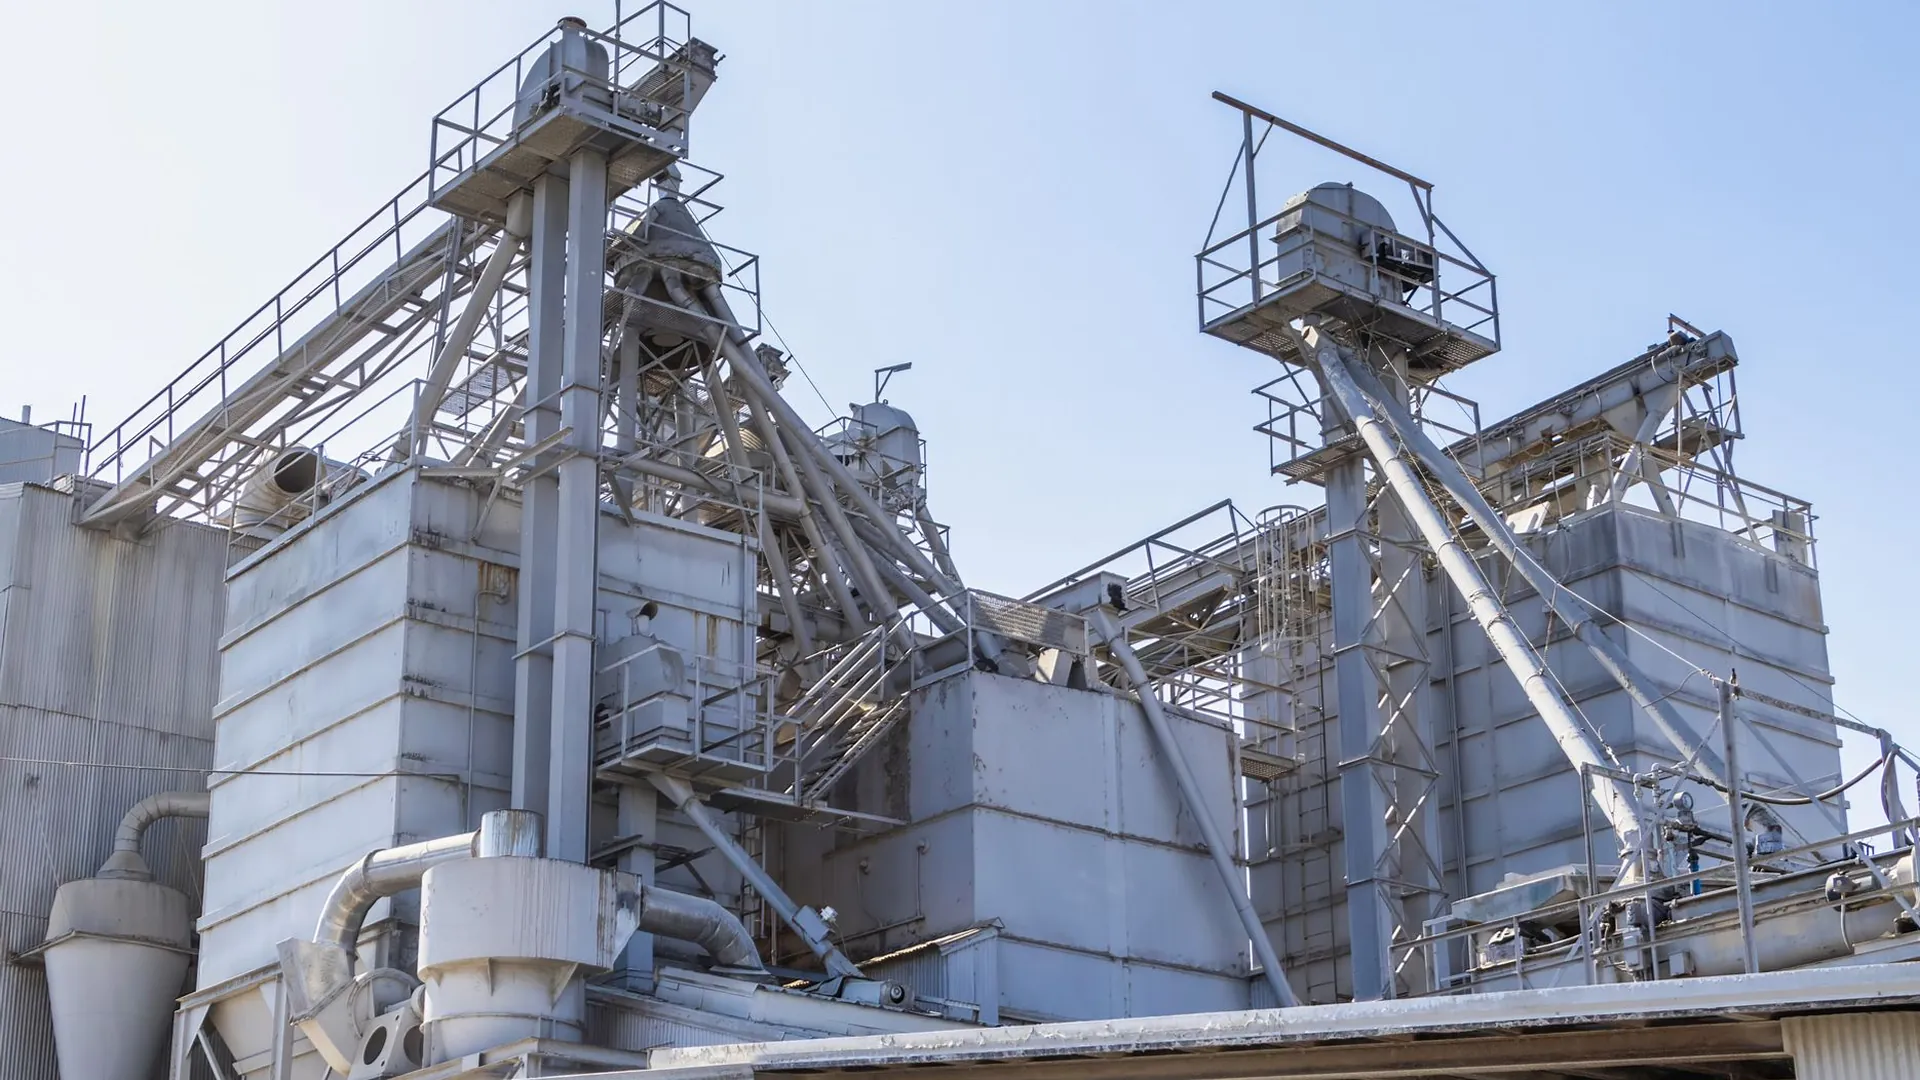
Clinker is ground with gypsum, fly ash or slag. The lab tests every batch before it is released.
Bagged or bulk, loaded from dry storage and unloaded where you need it on site.

What it saves
Blended cement uses less clinker, and less clinker means less water and less CO₂. Every product lists its saving per tonne against plain OPC. Here is the year so far.
The plant
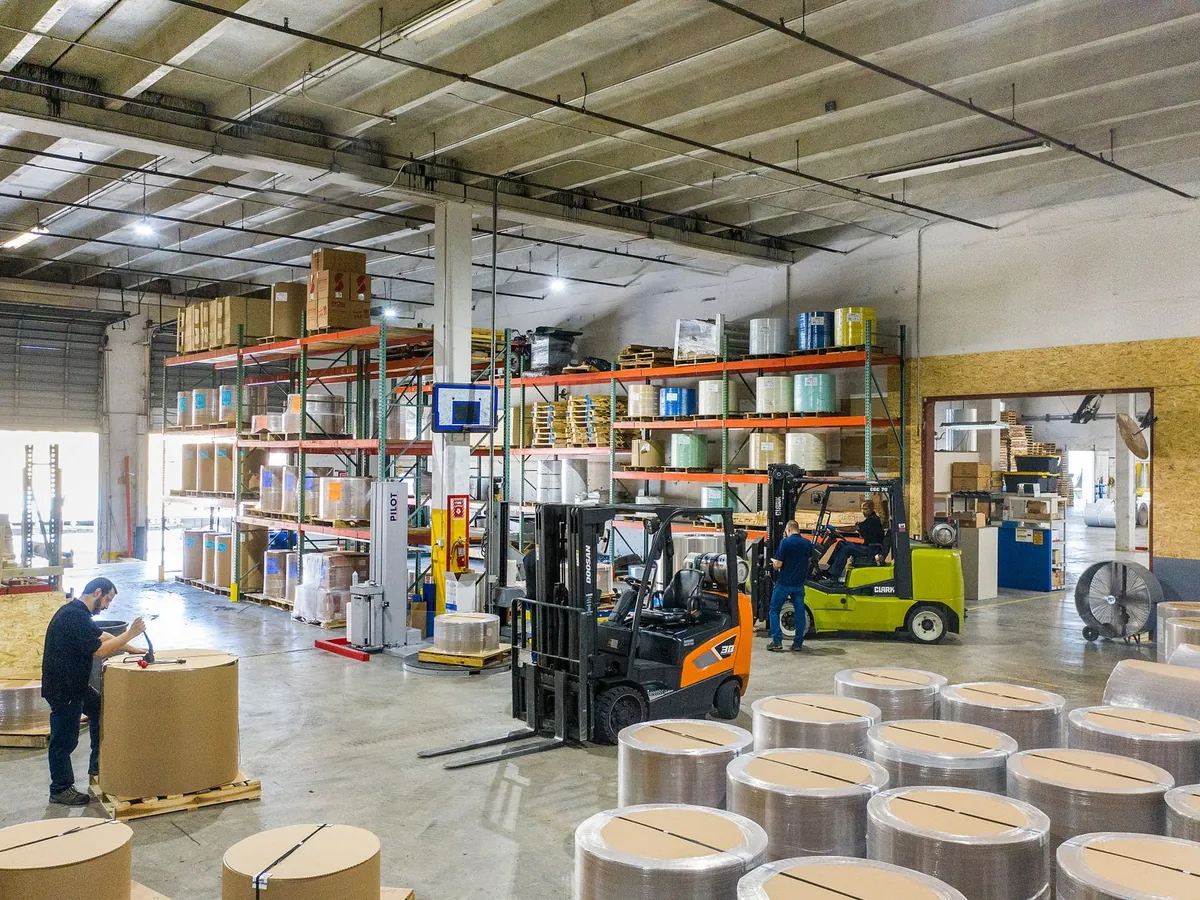
Two kilns, a vertical roller mill and a lab that runs every hour of every shift. Bagging and bulk loading sit side by side, so a pallet order and a tanker order leave from the same tested silo.